Description
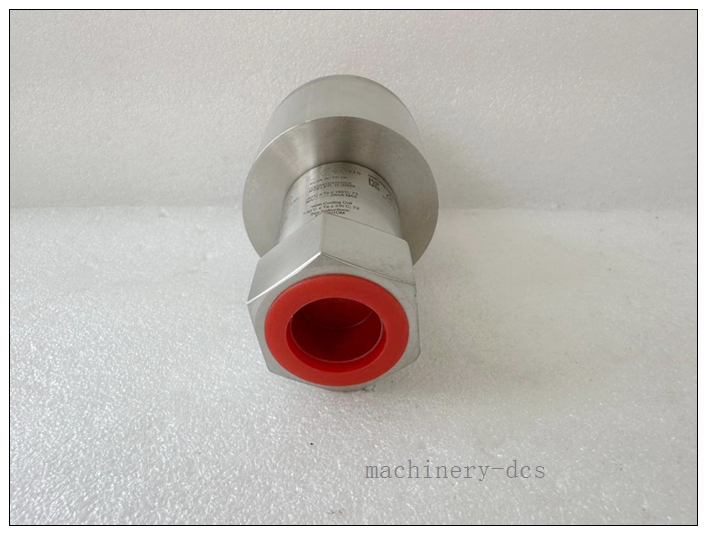
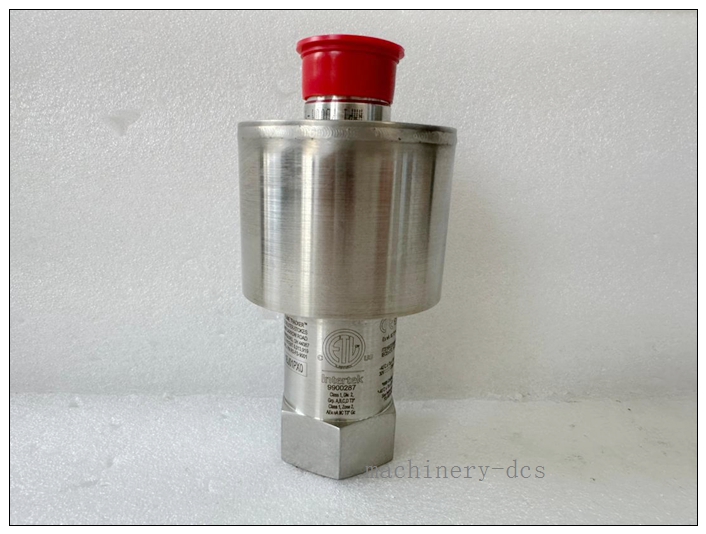
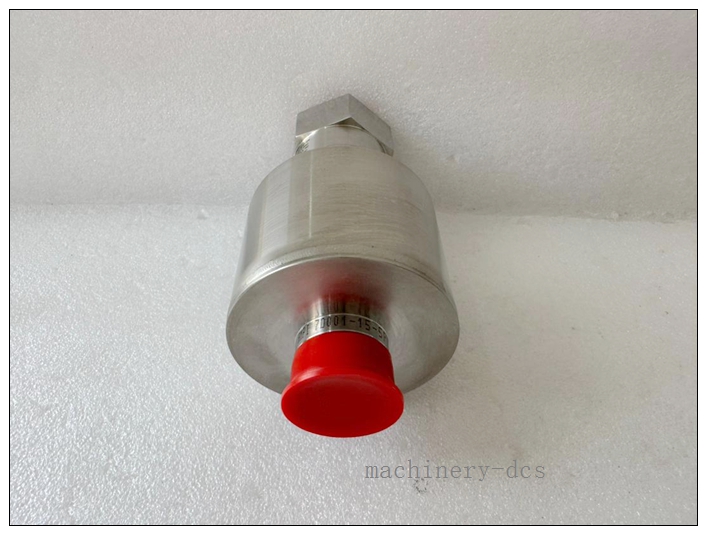
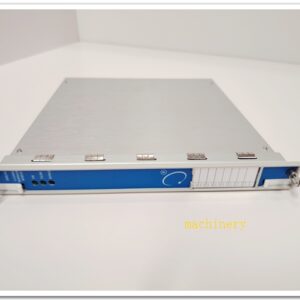
GE RS-FS-9001 Industrial Flame Detector Module
Executive Brief
The GE RS-FS-9001 is a high-performance industrial-grade flame detection module purpose-built for high-demand industrial safety monitoring scenarios. It adopts UV+IR dual-band detection technology, delivering fast and accurate flame or high-temperature gas detection in a wide temperature range and harsh media environments. It features rugged industrial construction, multiple output options and IP65~IP66 high protection rating, and is widely deployed in power plants, petrochemical facilities, continuous production lines and other mission-critical industrial sites.
RS-FS-9001
Core Technical Specifications
- Manufacturer: General Electric (GE)
- Exact Part Number: RS-FS-9001 (362A1052P004)
- Product Category: Industrial Flame Detector Module
- Detection Technology: Ultraviolet (UV) + Infrared (IR) dual-band detection
- Maximum Detection Range: 30 ft (≈ 9 m)
- Response Time: 10 microseconds (high-speed version) / < 2 seconds (standard version, some models < 1 second)
- Protection Class: IP65 to IP66
- Operating Temperature Range: -40°C to +85°C
- Storage Temperature Range: Matches the full operating temperature range
- Humidity Tolerance: 5%~95% non-condensing
- Detection Sensitivity: 0.1% FS (full scale)
- Output Signals: 4-20 mA analog, Modbus/RS-485 digital
- Power Supply: 24V DC ± 10% (220V AC version is also available)
- Physical Dimensions: Approximately 120mm x 90mm x 50mm (some models 200mm x 150mm x 50mm)
- Housing Material: Stainless steel or aluminum alloy
- Temperature Detection Range (temperature variant): 20 °C~1200 °C
- Pressure Measurement Range (multi-parameter variant): 0~2000 mbar
- Humidity Measurement Range (multi-parameter variant): 0%~100% RH
- MTBF Performance: Brushless DC motor (cooling variant) has a mean time between failures exceeding industry standard levels
- Compliance: Industrial-grade safety certification for hazardous area deployment
Key Features & Advantages
- Dual-band High-precision Detection: UV+IR dual-band detection technology effectively reduces false alarms caused by interference light sources, ensuring highly reliable flame identification.
- Ultra-fast Response Performance: The high-speed version achieves 10 microseconds response time, which can capture flame signals instantly and trigger protection actions immediately.
- Harsh Environment Adaptability: -40°C to +85°C wide operating temperature range, IP65~IP66 high protection rating and stainless steel/aluminum alloy housing, suitable for long-term stable operation in dusty, humid and vibration-prone industrial sites.
- Multiple Output Options: Supports both 4-20 mA analog signal and Modbus/RS-485 digital communication, seamlessly integrating with DCS, PLC and various industrial control systems.
- Flexible Power Supply Compatibility: 24V DC standard power supply with optional 220V AC version, adapting to different industrial field power supply conditions.
- Multi-parameter Expansion Capability: The multi-parameter variant integrates temperature, pressure and humidity measurement functions, realizing multi-dimensional environmental monitoring in one single device.
Typical Application Scenarios
- Power Plant Boiler Flame Monitoring: Core flame safety detection unit for boilers in thermal power plants, ensuring real-time flame status monitoring and protection.
- Petrochemical Furnace Safety Protection: Reliable flame detection module for heating furnaces, reaction kettles and other high-temperature equipment in refineries and chemical plants.
- Industrial Continuous Production Lines: Flame safety monitoring unit for high-temperature production processes in metallurgical, glass manufacturing and other continuous production lines.
- Oil & Gas Hazardous Area Monitoring: Rugged flame detection equipment for offshore oil platforms, oil depots and other flammable and explosive hazardous areas.
- Industrial Furnace Combustion Control: High-precision flame feedback sensor for industrial furnaces, kilns and combustion systems, supporting optimized combustion control.
RS-FS-9001
Related Supporting Product Model Display
- GE RS-FS-9000 Series Flame Detectors: Full range of RS-FS series flame detection products with different detection ranges and performance configurations.
- GE Industrial Safety Monitoring System: Upper-level safety monitoring platform that works with RS-FS-9001 to realize centralized flame status management and alarm processing.
- Industrial Explosion-proof Junction Boxes: Explosion-proof grade installation accessories suitable for RS-FS-9001 deployment in hazardous areas.
- GE DCS/PLC Communication Modules: Communication gateway modules that support Modbus/RS-485, realizing seamless data transmission between RS-FS-9001 and control systems.
Frequently Asked Questions
Q1: What detection technology does GE RS-FS-9001 use?
A1: It adopts UV+IR dual-band detection technology to achieve highly reliable flame identification and effectively reduce false alarms.
Q2: What is the maximum detection range of this flame detector?
A2: Its maximum effective detection range is 30 ft, approximately 9 meters.
Q3: What is the protection class of RS-FS-9001?
A3: Its housing protection class reaches IP65 to IP66, suitable for harsh industrial environments.
Q4: What output signals does this module support?
A4: It supports 4-20 mA analog signal and Modbus/RS-485 digital communication output.
Q5: What is the standard operating temperature range of RS-FS-9001?
A5: Its operating temperature range is -40°C to +85°C, adapting to extreme low and high temperature industrial scenarios.

 Start Chat

 Send an Email