When a communication module fails, or a replacement is specified with the wrong protocol, data exchange between PLCs, drives, HMIs, and field devices breaks down entirely. In multi-vendor environments, protocol mismatches are among the most common causes of integration delays and unplanned downtime.
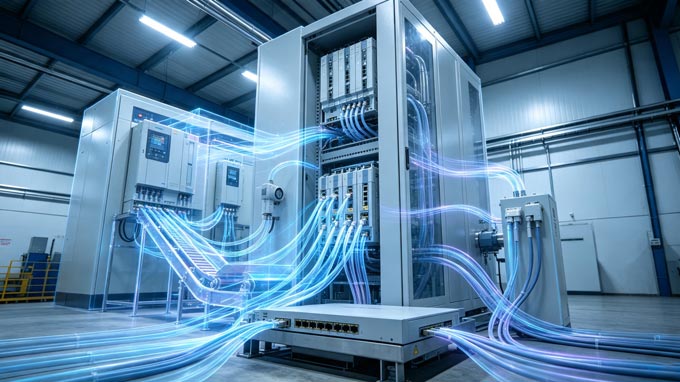
Industrial Communication Protocols and the Hardware Behind Them
How the three main protocols differ
- PROFIBUS: an RS-485 serial fieldbus up to 12 Mbps, offering deterministic, cyclic data exchange, widely installed in existing distributed-I/O and motion-control applications;
- PROFINET: Ethernet-based, supporting RT and IRT performance classes, suited to high I/O point counts and synchronized multi-axis motion, and able to bridge to legacy PROFIBUS segments through a gateway;
- EtherNet/IP: the CIP protocol over standard Ethernet, deployed widely in multi-vendor environments where interoperability across manufacturers matters most.
Five steps for choosing communication hardware on an aging system
- Identify the installed protocol from PLC documentation, network drawings, or device labels, rather than relying on the controller brand alone;
- Match the communication module strictly to the controller platform, cross-referencing the CPU series and rack slot, as modules are not interchangeable across platforms;
- Verify the physical layer: PROFIBUS uses shielded twisted-pair cable with DB9 connectors, while PROFINET and EtherNet/IP use RJ45 or M12 connectors; a mismatched interface will not connect;
- Confirm gateway requirements when bridging a PROFIBUS segment to an Ethernet network;
- Source hardware against the confirmed platform to avoid compatibility traps where a module looks the same but will not connect.
Many plants run both protocol families at once, using gateways to link older fieldbus segments to newer Ethernet segments without replacing installed field devices. Getting communication hardware right means matching the protocol, physical layer, and controller platform precisely, since a single mis-selection costs far more in downtime than the component itself.

 Start Chat

 Send an Email